-
Image

PM Package
Fix It Before It Stops
PES has spent years repairing furnace failures. We went back through them, worked out which modes keep recurring, and built the preventive maintenance package around stopping those specific ones.
Types of Maintenance
It is also called breakdown maintenance, which is a maintenance task that is performed in order to rectify and repair problematic systems and equipment. The purpose of corrective maintenance is to restore broken-down systems.
Usually, it is performed by the maintenance department, but for some equipment or spare part that can't be repaired by the maintenance department, PES Engineers are ready to support.
Please see the reference below:
It is a planned activity at regular intervals (time-based, periodic inspection, and overhaul) to eliminate causes of equipment failure and unscheduled interruptions to production, as an output of the manufacturing process design. [IATF, 2016]
According to the above requirement, the aim is to ensure maintaining the effectiveness of the production process. The concept is to check equipment and change key spare parts at the planned interval before equipment to be a breakdown.
In order to fully support customers, PES has launched a Preventive Maintenance (PM) Package for customers, see the information below:
An approach and set of techniques to evaluate the condition of in-service equipment by performing periodic or continuous monitoring of equipment conditions, in order to predict when maintenance should be performed.
This type of maintenance usually is integrated with the Internet Of Things (IoT). Our engineering team is able to support for RETROFIT of some furnaces through extensive discussion and consultation with PES Engineers, such as for SMART MANUFACTURING.
While for a new furnace, our furnace partner: IPSEN is able to supply a furnace equipped with PDMetrics(R) Software.
Why Furnace Preventive Maintenance is Necessary ?
Many customers may never think about the necessity of Preventive Maintenance as they will have an overhaul at the end of the year or repair the furnace when it is broken, but what they do not know is that this proactive action of Preventive Maintenance for your furnace is very beneficial for your furnace maintenance team. So, the benefit of our PM Packages are:
- Avoiding Breakdown that can cause disruption in the production schedule
- To make sure that parts for maintenance are always available or delivered on time
- Avoiding unsatisfied customers due to the problem in the supply chain, that reduced your reliability.
- Avoiding any accident or injury caused by furnace problems
- Avoiding costly repair due to undetected & continuous furnace problems.
Why It Matters
What Preventive Maintenance Prevents

Avoiding Breakdown
Breakdowns disrupt the production line, and the disruption usually costs more than the repair.

Parts On Hand
Making sure the parts maintenance needs are available when the work is scheduled, not ordered after a failure.

Keeping Delivery Promises
Avoiding unsatisfied customers when a production problem turns into a missed delivery.

Safety
Avoiding accidents and injuries caused by furnace problems that were visible before they became dangerous.

Avoiding Costly Repair
Undetected wear continues, and the repair bill grows with it. Finding it early is the cheaper option.

Reactive, Preventive, Predictive
PES works across all three: corrective repair when something fails, scheduled preventive work, and predictive maintenance from condition data.
Bright Annealing Furnaces
Furnace Sections for PM:
- Inlet
- Charge Vacuum
- Heating Zone
- Degassing Room
- Cooling Zone
- Discharge Vacuum
- Outlet
- Door 1, 2, 6, 7
- Gas Generator
Total Working Time: 8 Days
Required Working Condition:
- Stop the Furnace
- Furnace temperature should be below 50 C
- No Load
- Overhead Crane supported by customer
- Customer Supplying grease
- Not Including Repair & Spare Parts
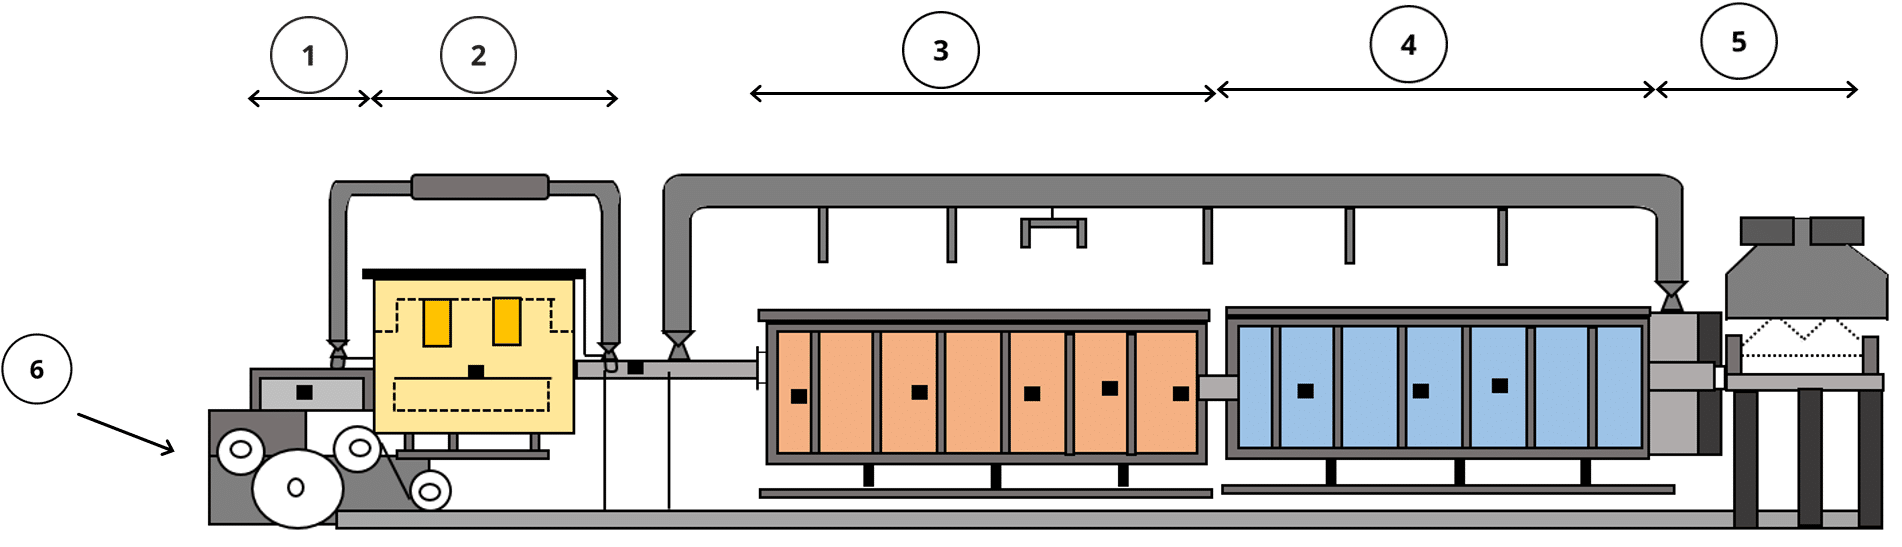
Mesh Belt Aluminum Brazing Furnace
Furnace Sections for PM:
- Entrace Chamber
- Drying Oven Zone
- Preheating & Brazing Zone
- Cooling Zone
- Exit Zone
- Mesh Belt & Driving Unit
- Control Panel
Total Working Time: 2 - 3 Days
Required Working Condition:
- Stop the Furnace
- Furnace temperature should be below 50 C
- No Load
- Overhead Crane supported by customer
- Customer Supplying grease
- Not Including Repair & Spare Parts
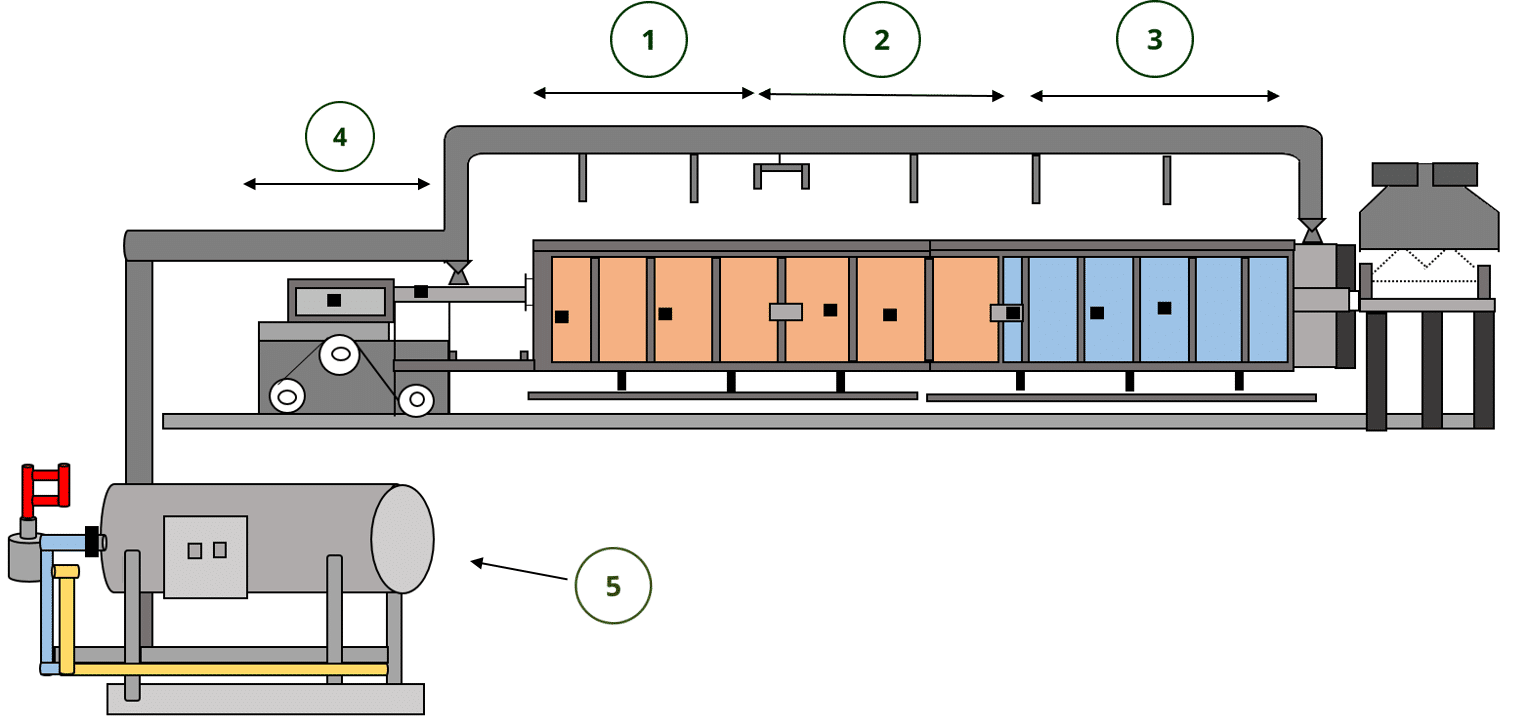
Mesh Belt Copper Brazing Furnace
Furnace Sections for PM:
- Preheating Zone
- Heating Zone
- Cooling Zone
- Mesh Belt & Driving Unit
- Endothermic Unit Gas (DX Gas Generator)
- Control Panel
Working time: 7 Days
Required Working Condition:
- Stop the Furnace
- Furnace temperature should be below 50 C
- No Load
- Overhead Crane supported by customer
- Customer Supplying grease
- Not Including Repair & Spare Parts
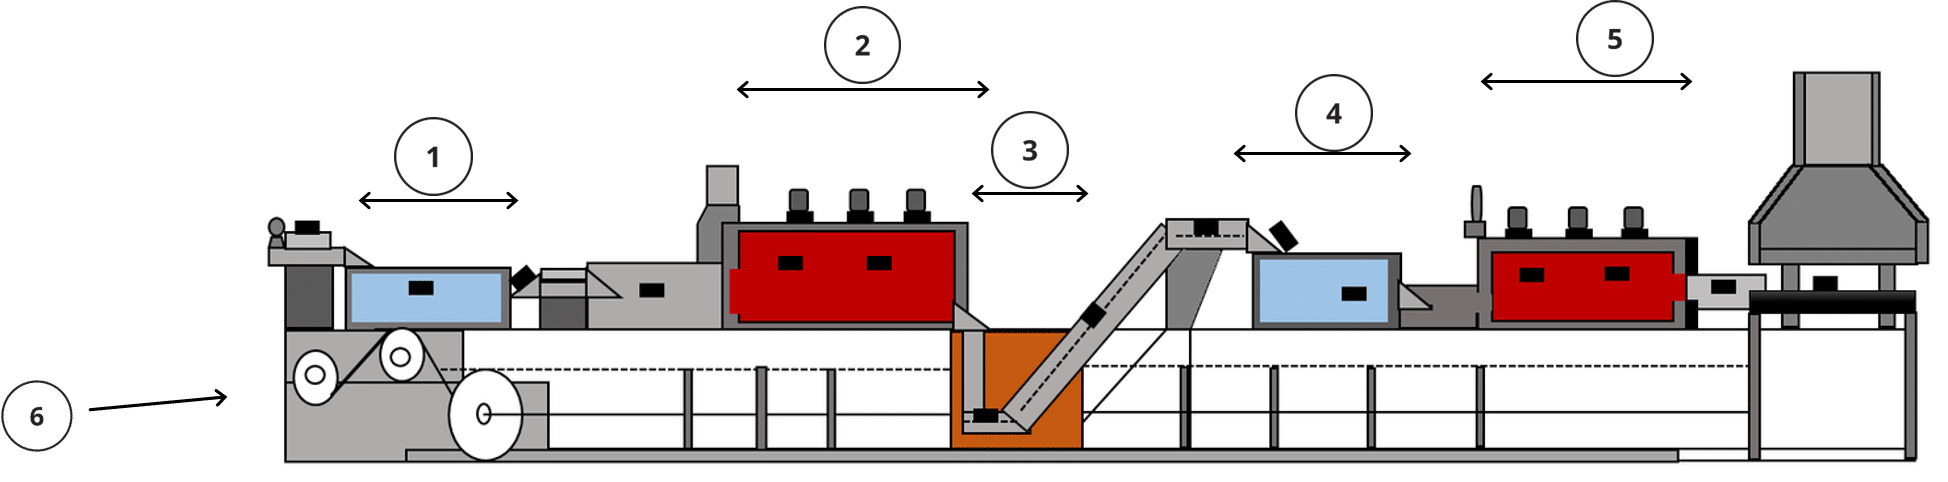
Mesh Belt Hardening, Quenching, Tempering Furnace
Furnace Sections for PM:
- Pre-washer
- Hardening Furnace
- Quenching Oil Tank
- Post - Washer
- Mesh Belt & Driving Unit
- Tempering Furnace
- Control Panel
Working time: 4 - 5 Days
Required Working Condition:
- Stop the Furnace
- Furnace temperature should be below 50 C
- No Load
- Overhead Crane supported by customer
- Customer to empty the quenching media
- Not Including Repair & Spare Parts
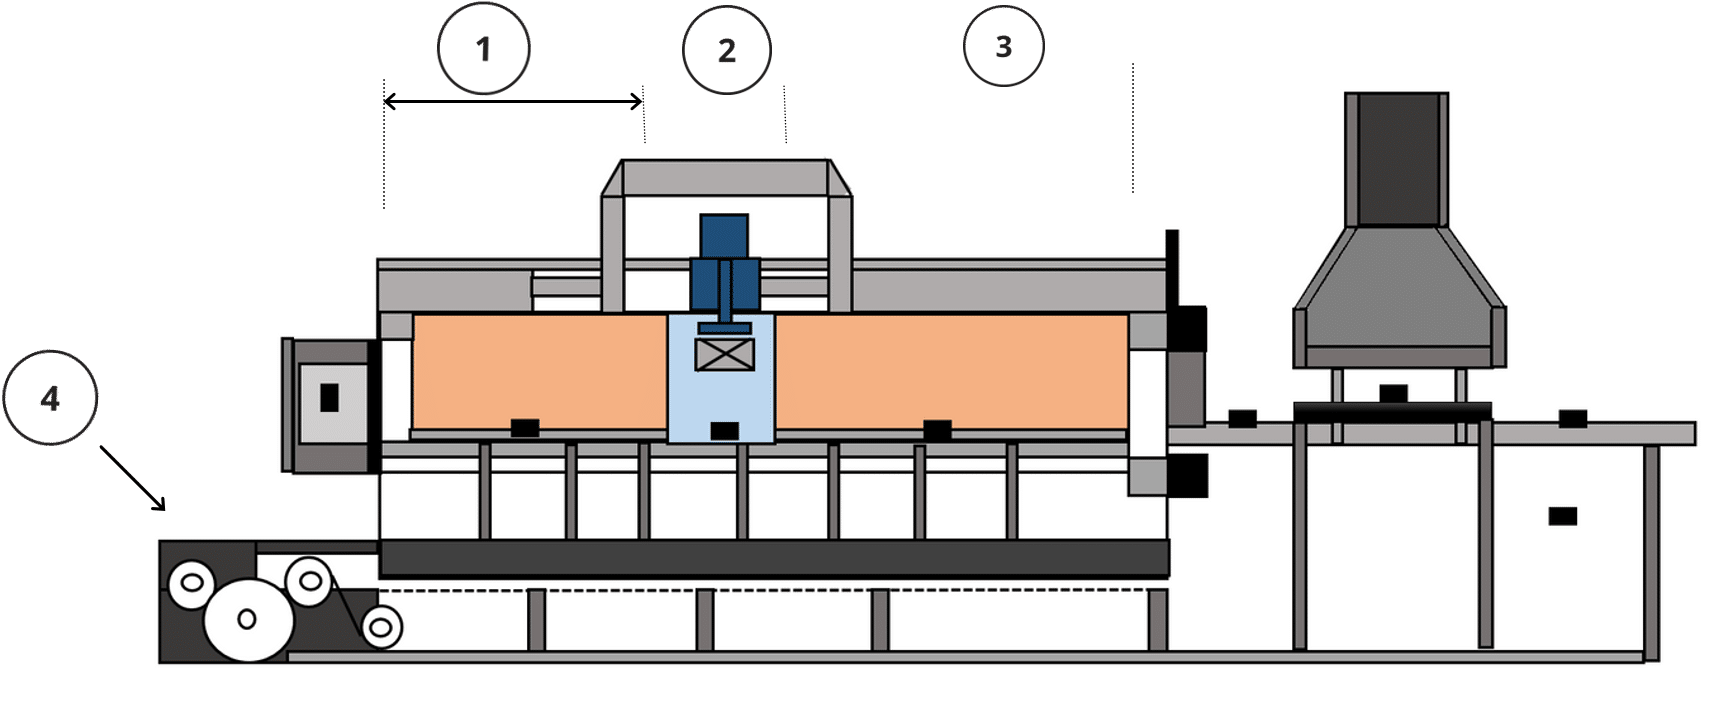
Mesh Belt Normalizing Furnace
Furnace Sections for PM:
- Soaking Zone
- Cooling Zone
- Isothermal Zone
- Mesh Belt & Driving Unit
- Control Panel
Working time: 2 - 3 Days
Required Working Condition:
- Stop the Furnace
- Furnace temperature should be below 50 C
- No Load
- Overhead Crane supported by customer
- Customer to empty the quenching media
- Not Including Repair & Spare Parts
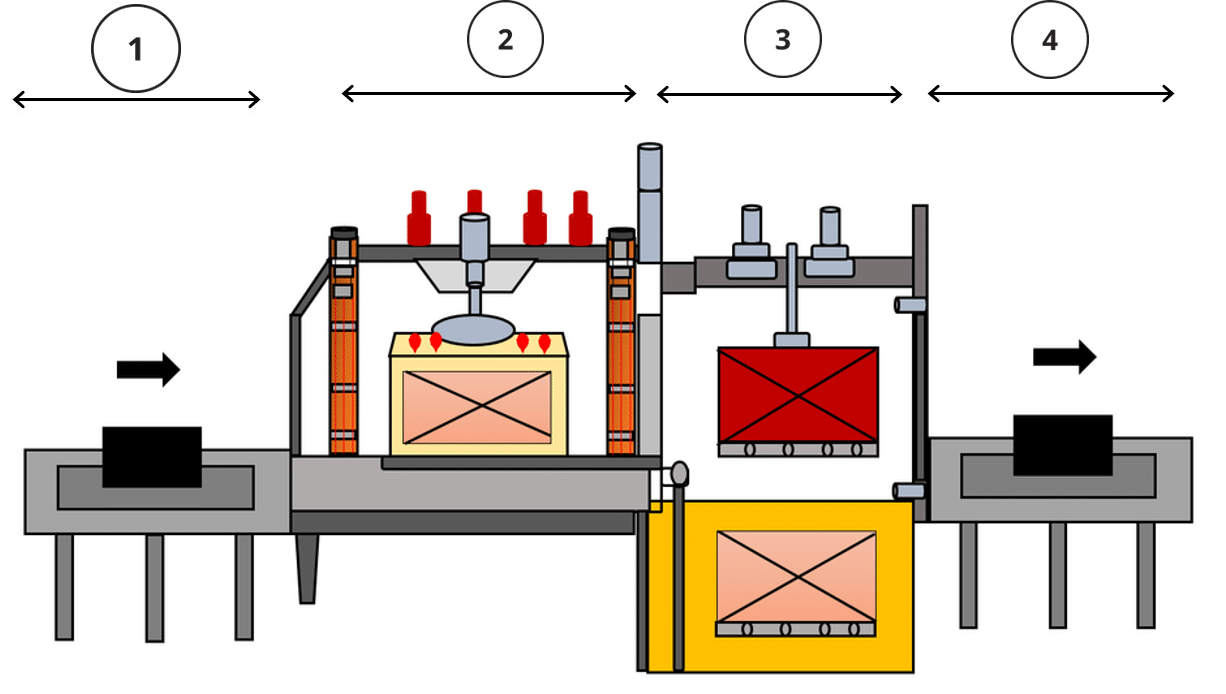
Batch Type Carburizing Furnace
Furnace Sections for PM:
- Loader Unit
- Heating Zone
- Quenching Oil Tank
- Exit Zone
- Control Panel
Working time: 3 - 4 Days
Required Working Condition:
- Stop the Furnace
- Furnace temperature should be below 50 C
- No Load
- Overhead Crane supported by customer
- Customer to empty the quenching media
- Not Including Repair & Spare Parts
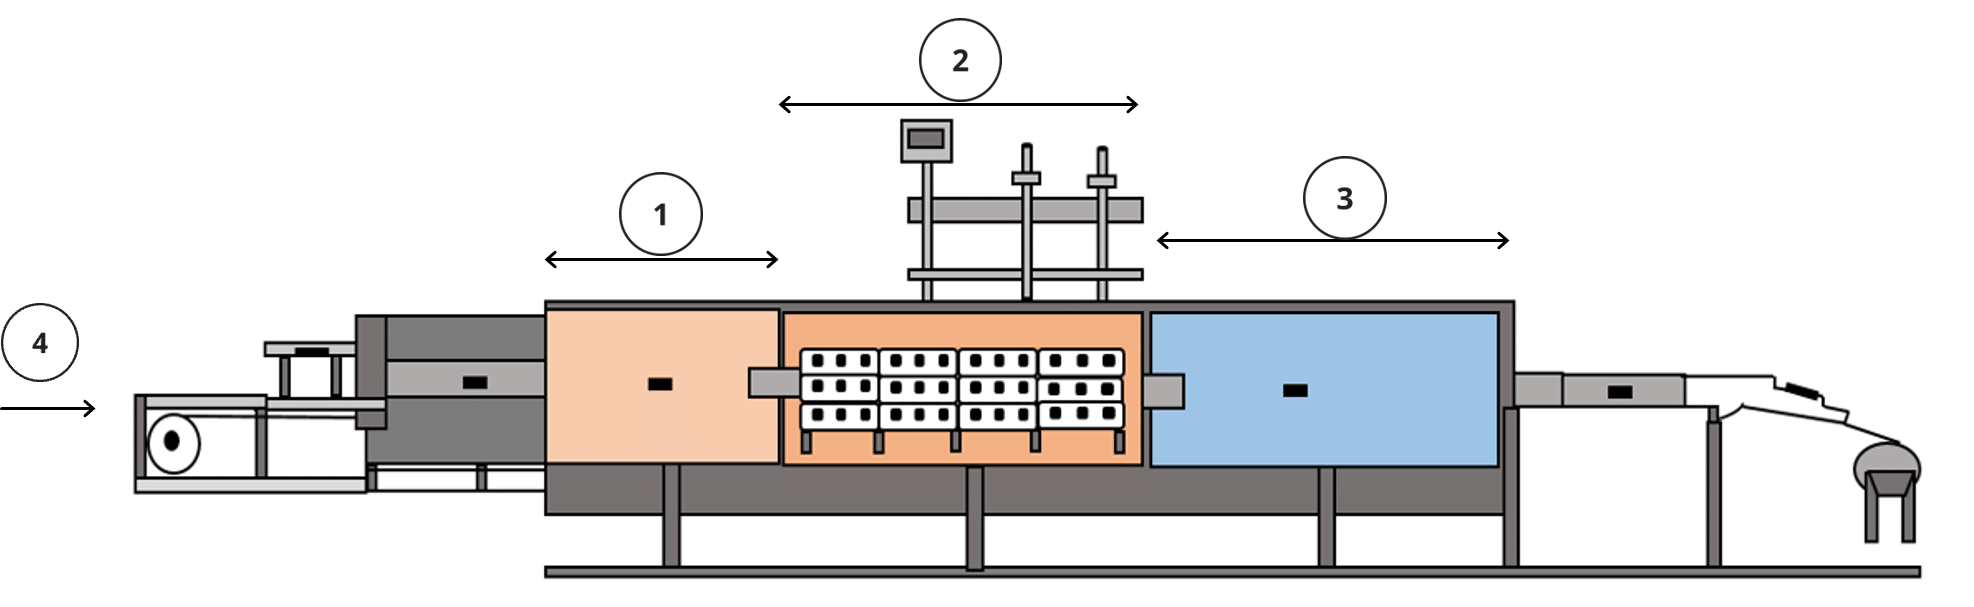
Mesh Belt Type Sintering Furnace
Furnace Sections for PM:
- Pre-Heating Zone
- Heating Zone
- Cooling Zone
- Mesh Belt & Driving Unit
- Control Panel
Working time: 2- 3 Days
Required Working Condition:
- Stop the Furnace
- Furnace temperature should be below 50 C
- No Load
- Customer to empty the quenching media
- Not Including Repair & Spare Parts
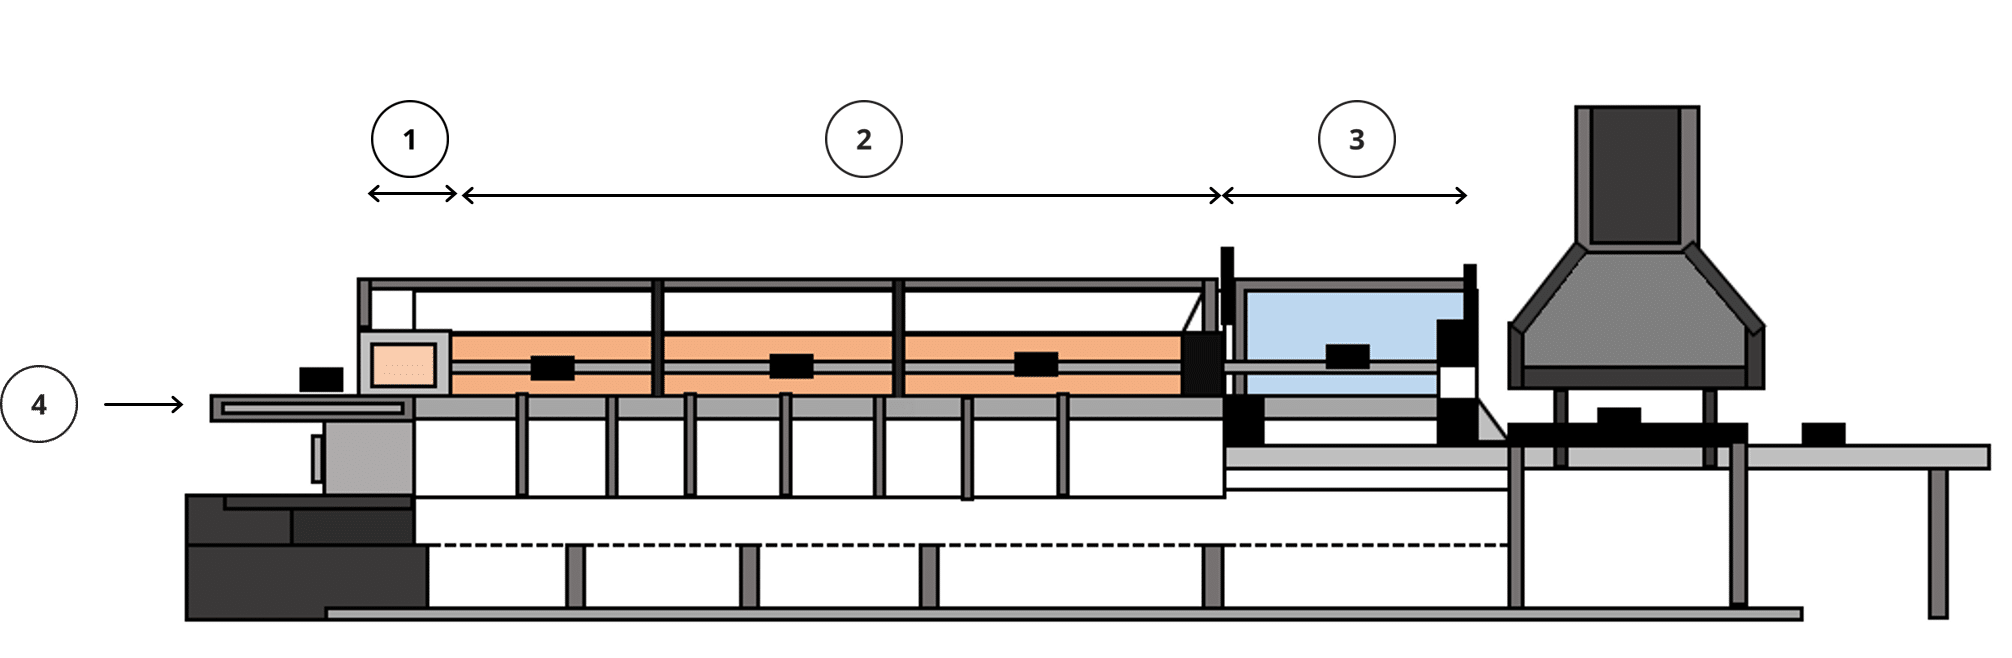
Pusher Type Sintering Furnace
Furnace Sections for PM:
- Pre-Heating Zone
- Heating Zone
- Cooling Zone
- Pusher Unit
- Control Panel
Working time: 2 - 3 Days
Required Working Condition:
- Stop the Furnace
- Furnace temperature should be below 50 C
- No Load
- Customer to empty the quenching media
- Not Including Repair & Spare Parts
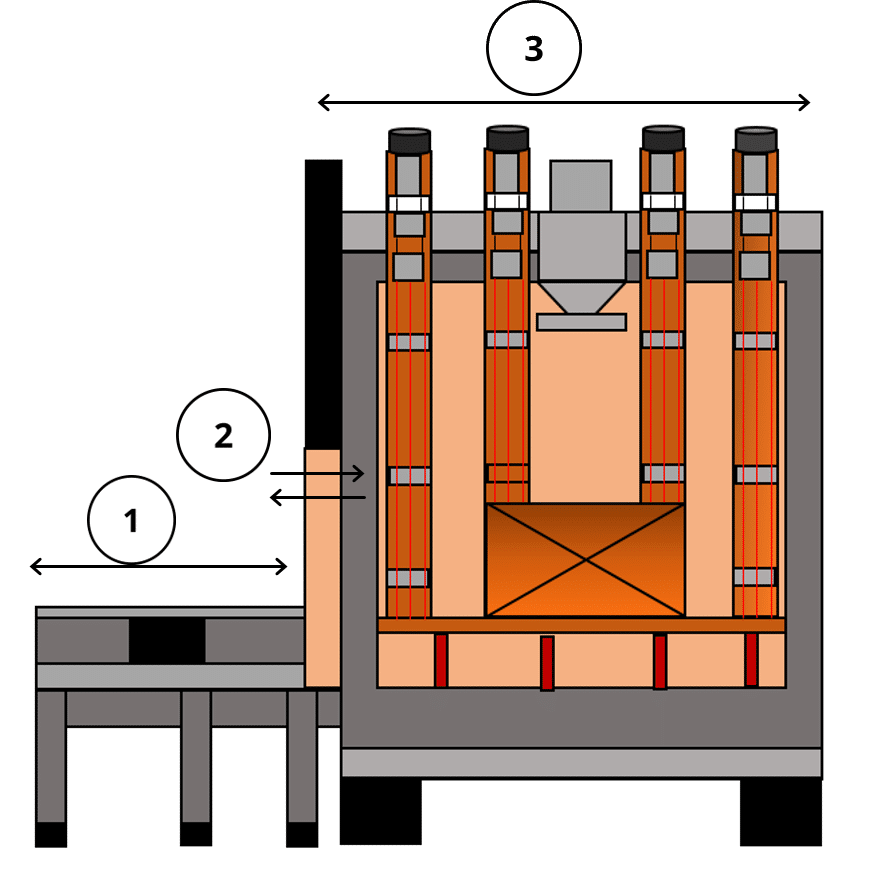
Batch Type General Furnace
Furnace Sections for PM:
- Loader Unit
- Entrance and Exit Zone
- Heating Chamber
- Control Panel
Working time: 1- 2 Days
Required Working Condition:
- Stop the Furnace
- Furnace temperature should be below 50 C
- No Load
- Customer to supply overhead crane
- Customer to empty the quenching media
- Not Including Repair & Spare Parts
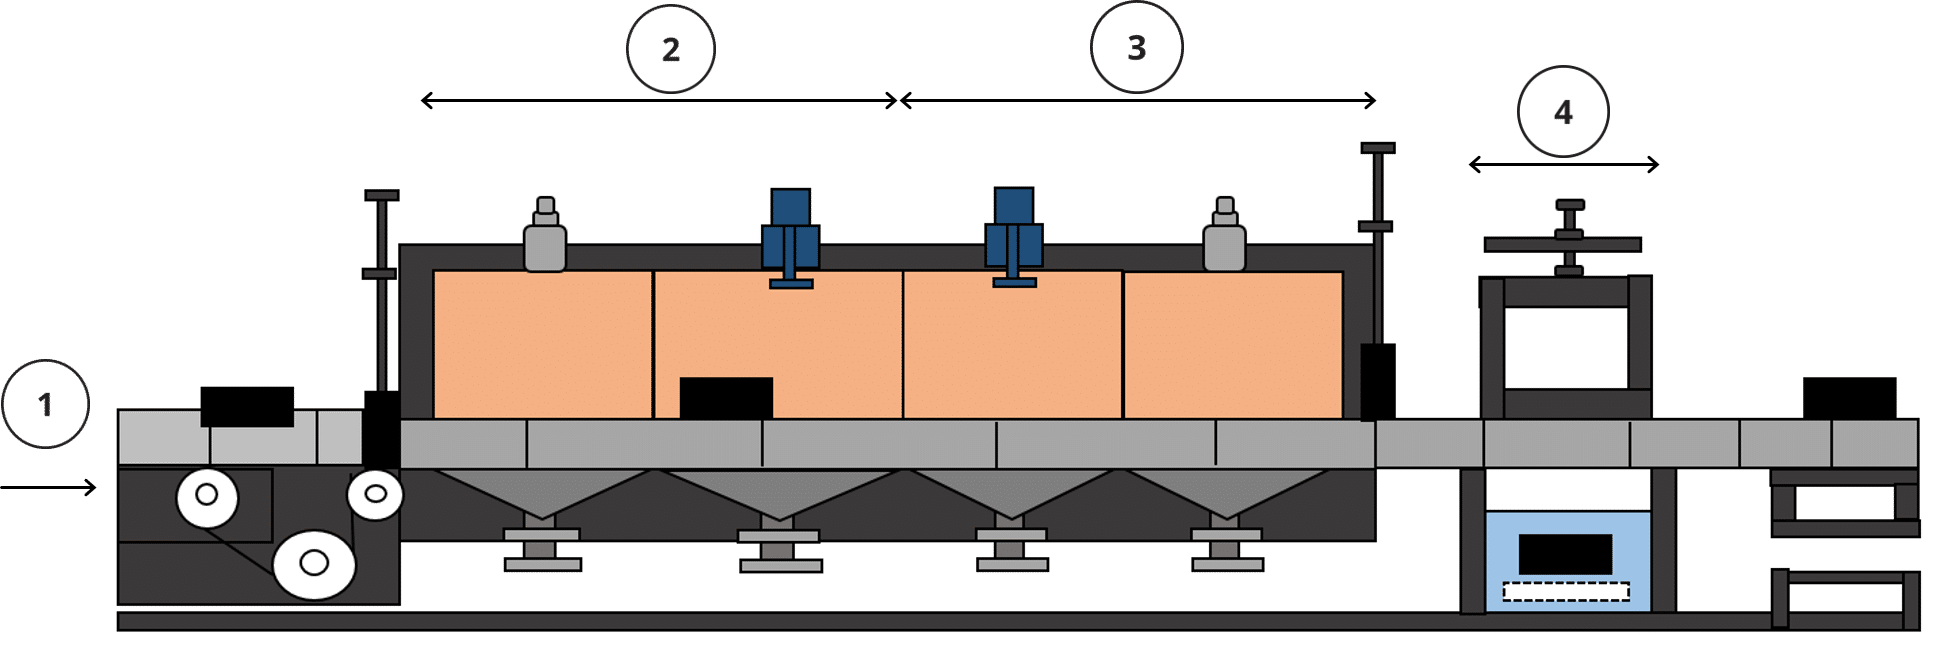
Solution Heat Treatment Furnace
Furnace Sections for PM:
- Loader Unit
- Pre-Heating Zone
- Heating Zone
- Quenching Water Tank
- Control Panel
Working time: 3- 4 Days
Required Working Condition:
- Stop the Furnace
- Furnace temperature should be below 50 C
- No Load
- Customer to empty the quenching media
- Not Including Repair & Spare Parts
For more information, do not hesitate to contact us here or contact our LINE & WhatsApp
Click here for more details of PM package:
-
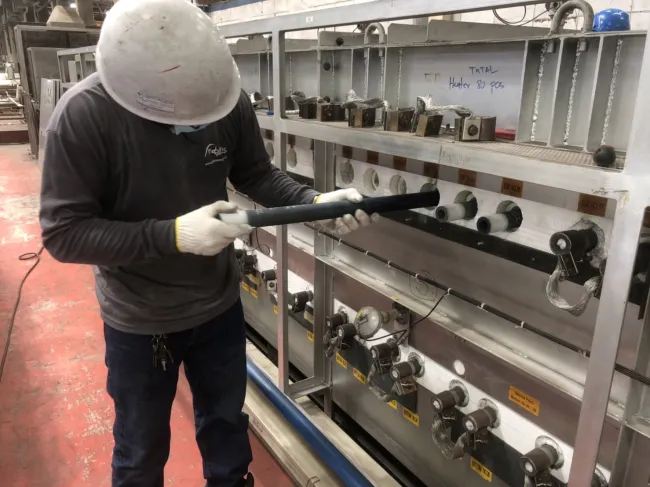
Case Study 1
SiC Heater "EREMA" Installation & Thrystor's Adjustment for Bright Annealing Furnace
Read Full Case StudyProlific Engineering and Service Co., Ltd (PES) is capable to offer multiple services including the tuning of Bright Annealing Furnace. Bright Annealing Furnace requires high temperature for its operation, thus Silicon Carbide (SiC) heater …
-
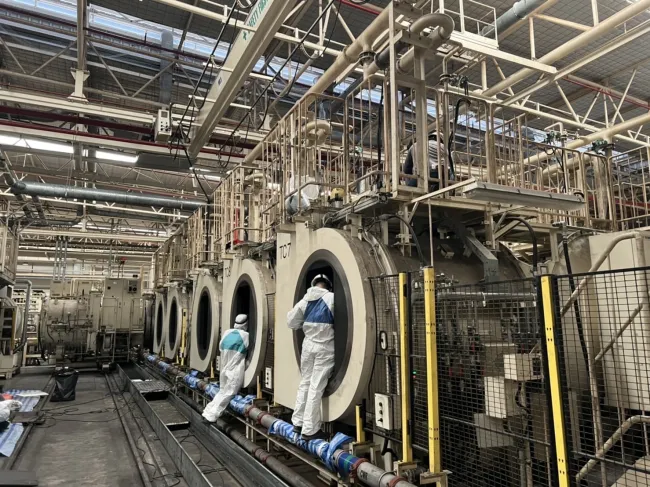
Case Study 2
Vacuum Furnace Repair by PES Team
Read Full Case StudyOur Prolific Engineering and Services (PES) team have successfully completed a repair job for multiple Vacuum Furnaces in one of our automotive part maker customer.
-
-
-
-